
- Calibrated metrology — Hexagon CMMs, vision and gear measuring machines, laser microscope, profilometer.
- SPC with measured Cpk — Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) on a real 76.1–76.5 mm characteristic; Ppk ≥ 1.67 initial · Cpk ≥ 1.33 in production.
- XRF at the door — every incoming lot checked against its mill certificate before cutting.
- Lot-level traceability — material, machine, operator and inspection recorded in MES/ERP.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
What is the first thing an auditor checks in quality?
Calibration. An inspection instrument that has not been calibrated on schedule produces numbers that look precise and are wrong, and a wrong number is worse than no number because it is confident. So the first quality question is not "do you have a CMM" but "show me the calibration records for it." A quality system that cannot produce calibration records is a quality system in name only.
This is why the audit starts at the inspection bench, not the machines. The inspection bench is the part of the factory that checks the rest of it, and its credibility is the credibility of every measurement that leaves the building. The calibration records are the first document requested, and they are produced on request.
The record to ask for is the one that names each instrument, its last calibration date, and its next due date. An instrument with a lapsed date does not produce wrong numbers loudly; it produces numbers that look precise and drift without warning, and a drifted CMM will pass parts that a calibrated one would fail. That is why the calibration record is the first document in the audit, and why a quality system that cannot produce it is a quality system in name only.
Which instruments verify the dimensions?
The dimensional claim — ±0.003 mm on CNC milling, ±0.002 mm on CNC turning, ±0.002 mm for grinding — is only as real as the instruments that check it. The bench has to be the same class of equipment a buyer would use to audit the shop, because a tolerance that cannot be measured cannot be verified.
- Hexagon GLOBAL S CMMs (2) for dimensional verification, with ranges of 800 × 600 × 600 and 900 × 1500 × 800.
- Vision measuring machines (Hexagon OPTIV and VIEWMAX E) and a gear measuring center for geometry.
- KEYENCE VK-X3000 laser microscope and SURFCOM 1800D profilometer for surface finish and profile.
- Height gauges (Mitutoyo and TESA), contour and roughness testers for hand verification.
Two of those instruments exist specifically for the surface, and they answer the finish half of the tolerance claim. The laser microscope and the profilometer turn a surface-finish call-out like Ra 0.8 µm into a measured trace rather than a visual guess, because a bearing seat that looks smooth and a bearing seat that measures Ra 0.8 µm are not the same thing, and only one of them survives contact with the mating part.
How is the tolerance proven, not just claimed?
By a measured number, not a sentence. The question an auditor asks is "show me an SPC chart or a CMM report from a real job," and the answer is either a number or an excuse. A capability statement that says "we hold tight tolerances" proves nothing; a Cpk value from a real characteristic proves something you can check against the print.
On a representative length characteristic of 76.1–76.5 mm, this factory's SPC record shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), against an initial-study target of Ppk ≥ 1.67 on key characteristics and a production target of Cpk ≥ 1.33. That number comes from 25 subgroups of 4 parts each, with X̄ = 76.393 and R̄ = 0.04 — a measured result from a real job, which is exactly the kind of evidence you should demand from any machining factory before ordering.
| Cpk value | What it means | Where it applies |
|---|---|---|
| 1.33 | Process runs roughly four sigma inside the band | General characteristics |
| 1.67 | Roughly five sigma inside the band | Key characteristics |
| 1.851 (one characteristic on one part, not a blanket capability claim) (measured here) | Comfortably inside the key-characteristic floor | The 76.1–76.5 mm length characteristic |
Read Cpk as a statement about the spread, not about one part. The number is calculated from subgroups measured across a run, so it describes how much room the process leaves between its natural variation and the tolerance walls. A Cpk of 1.0 means the process just fits the tolerance with nothing to spare; each step above that buys margin against tool wear, material variation and thermal drift. The measured 1.851 (one characteristic on one part, not a blanket capability claim) says the process is running well inside the band, which is exactly what the subgroups behind it must show.
How is incoming material checked?
At the door, before it reaches a machine. The most expensive defect in machining is a perfect part made from the wrong material — a failure that is silent through machining and inspection and only surfaces later, in your assembly or in the field. The only place to prevent it is the receiving step, and the only way to catch it reliably is a composition check against the certificate.
This factory checks every incoming lot by XRF against its mill certificate, so a mixed or mislabeled alloy is caught before cutting. The XRF (iCHEQ) spectrometer reads the material composition, which is then compared against the certificate that arrived with the bar. That single step converts "we trust the supplier's label" into "we verified the supplier's label," which is the whole point of incoming inspection.
How are parts traced back to the raw material?

Traceability is the answer to the question every quality manager dreads: if a part fails, can you tell me why, and which other parts are affected? A factory without traceability can only guess at both; a factory with it can isolate the impact to a specific lot, machine and operator, and contain the problem instead of firing it in all directions.
This factory's MES/ERP system records the full chain on every lot: raw material source and usage, process parameters, machine data, production batch, machining time, operator and inspection results. When a non-conformance surfaces, the answer is specific rather than a shrug — which lot, which machine, which operator — and that is the discipline IATF 16949 audits look for, running on every job, not only the automotive ones.
Traceability also changes what a failure costs. Without it, one bad part can mean scrapping or recalling an entire shipment, because no one can say which parts share the bad lot. With it, the impact is contained to the parts that actually ran through the suspect machine or material — a difference that turns a recall into a targeted replacement. That is the economic case for the record, and it is why the audit treats traceability as a cost control, not a paperwork exercise.
What does the SPC and process control actually look like?

Process control is documented discipline, not a slogan. For a real customer program this factory holds a complete APQP/PPAP package: a process flow chart from incoming inspection through machining, post-processing, heat treatment, cleaning, final inspection and packing; a control plan naming the critical characteristics and inspection frequency; a PFMEA mapping the failure modes and their mitigations; and the SPC chart that proves the process stayed in control. These are real documents from a real job, not template pages.
Why this matters to a buyer: an APQP/PPAP package is evidence that the factory can plan and control a process to automotive standards — the same discipline that protects any regulated or high-value part. Ask to see a sample of it during your audit; a genuine factory can produce one, a trading desk cannot.
What documents ship with the parts?
The evidence should travel with the product. When parts ship, the CMM inspection reports, SPC control charts and material certificates go with them, so your own incoming inspection can be checked against a documented baseline. Every critical dimension carries a measured value rather than a pass/fail flag, which is the difference between "we checked it" and "here is what we measured."
This closes the loop on the audit: the same evidence you request before ordering is delivered with the order. A factory that gives you the measurements on the way out is a factory that has nothing to hide in them, and that transparency is, in itself, the strongest signal of a real quality system.
Which certifications back the quality system?
Certifications are the third-party-surveilled proof that the quality system is not just internal good intentions. They carry numbers you can check with the registrar, and they carry scopes that tell you exactly what is covered, and what is not.
| Standard | Certificate number | Scope |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
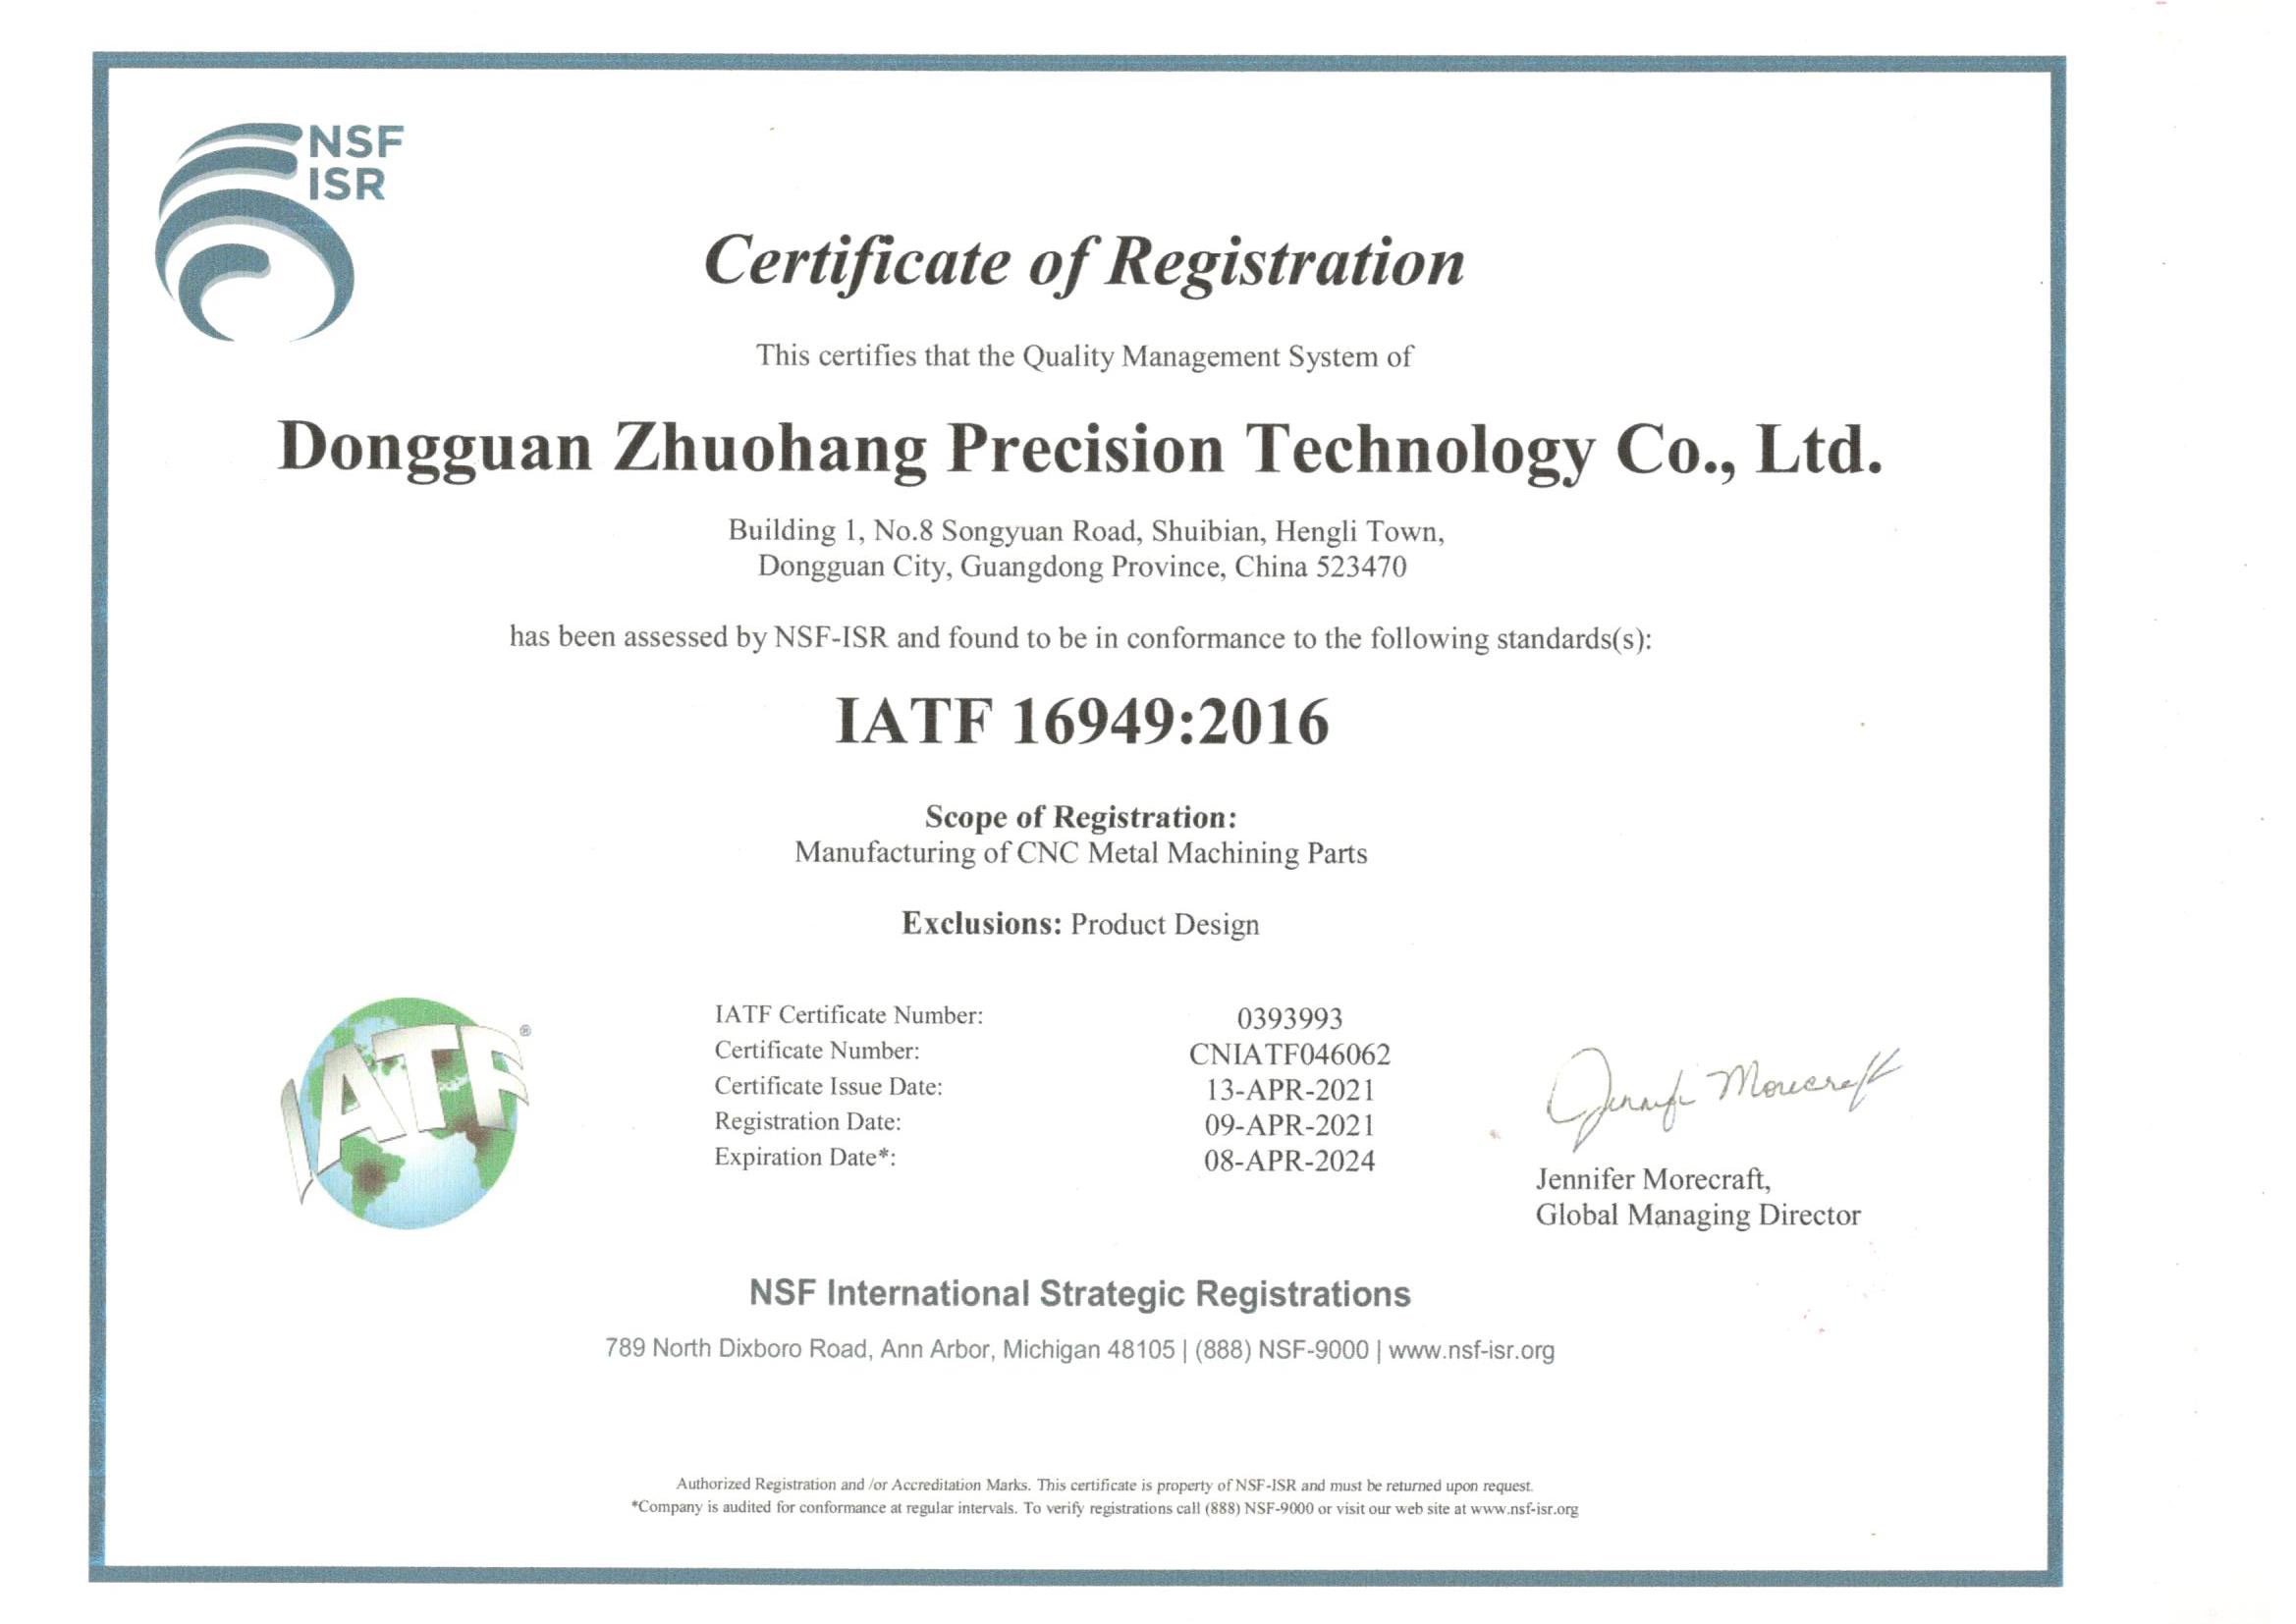
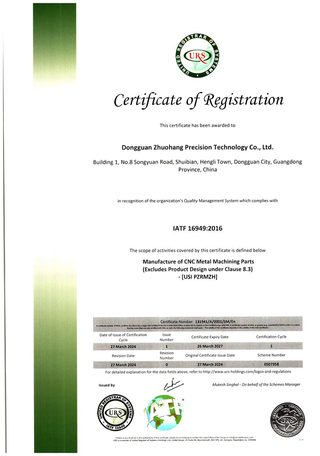
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
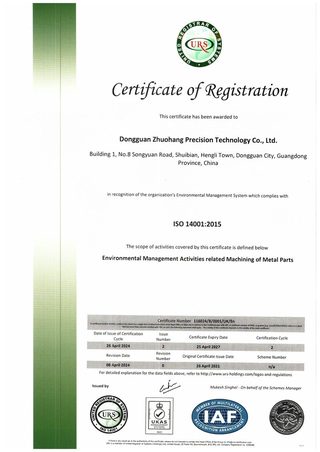
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Honest scope note: IATF 16949 excludes product design under Clause 8.3. This is a build-to-print factory — it machines to your print, it does not own the design responsibility. If your program needs design ownership, that is scoped separately and stated up front rather than over-promised.
How does SPC catch a drift before it becomes a defect?
SPC earns its keep by catching a process that is still in tolerance but already moving. A single part can be in spec while the tool is wearing, the temperature is climbing, or the operator has drifted from the setup, and the chart is what shows the trend before the parts cross the line. Control limits drawn around the process mean are the tripwire: when the plotted subgroups start hugging one limit, or run consistently on one side of the mean, the chart flags it while the parts are still good.
The practical question for you is whether the shop reacts to the chart or just files it. A real SPC program has a reaction plan — when the chart signals, someone checks the tool, the fixture or the offset, and the record shows what was done. A chart with no reaction plan is a recording of history, not a control system, and the audit should ask which one the factory runs.
What does first-article inspection add to the loop?
First-article inspection is the gate between the first cut and the full run. Before a batch starts, the first part off the machine is measured against every dimension on the print and the result is recorded against the drawing, so a wrong setup is caught on one part instead of a thousand. In an audited factory, the FAI report is the document that says the machine is set to make your part, not a part that resembles yours.
FAI and SPC are complementary, not interchangeable. FAI confirms the setup is right at the start; SPC confirms the process stays right across the run. A shop that offers one without the other is covering half the risk — the first part can be perfect while the process drifts, or the process can be stable while the first part was never verified against the print. The audit asks for both, because together they bracket the entire production window.
What this shop actually runs
We machine every part in our own 6,800 m² plant in Dongguan, China, on 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Cut on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Cut on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Cut on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Cut on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Cut on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Audit the quality system before you order
Send your drawing to [email protected] or call +86 13126536955 — calibration, SPC and traceability evidence on request.
Frequently Asked Questions
How is quality audited at a machining factory?
In short, Quality is audited the way an auditor audits it: through documents and instruments, not adjectives. The checklist covers calibration records for the inspection bench, CMM and SPC evidence that a tolerance is actually held, XRF verification of incoming material, and lot-level traceability that links a part back to its raw material, machine and operator.
What instruments verify the dimensions?
In short, Two Hexagon GLOBAL S CMMs handle dimensional verification, supported by a gear measuring center and vision measuring machines, plus a KEYENCE VK-X3000 laser microscope and a SURFCOM 1800D for surface finish and profile. Every critical dimension is measured on this bench, so a part is verified rather than assumed correct.
What does the SPC data show?
In short, On a representative length characteristic of 76.1–76.5 mm, the SPC record shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), against an initial-study target of Ppk ≥ 1.67 on key characteristics and a production target of Cpk ≥ 1.33. That is a measured result from a real job, not a capability claim, and it is the kind of number an auditor asks to see.
How is incoming material verified?
In short, Every incoming lot is checked by XRF against its mill certificate before it reaches a machine, so mixed or mislabeled alloy is caught at the door. This prevents the most expensive defect in machining — a perfectly machined part made from the wrong material — which is silent until it fails in your assembly.
Can parts be traced back to the raw material?
In short, Yes. An MES/ERP system records the full chain on every lot: raw material source and usage, process parameters, machine data, production batch, machining time, operator and inspection results.
What documents ship with the parts?
In short, CMM inspection reports, SPC control charts and material certificates ship with the parts. Every critical dimension carries a measured value rather than a pass/fail flag, giving the buyer documented evidence of what was actually received, which is what an incoming inspection on your side can be checked against.
Which certifications back the quality system?
In short, Three, with verifiable numbers: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En) and ISO 14001:2015 (116024/B/0001/UK/En), all issued by URS. IATF 16949 scope excludes product design under Clause 8.3, so the operation is build-to-print.
Is there evidence of automotive-grade process control?
In short, Yes. A complete APQP/PPAP package exists for a real customer program — process flow chart, control plan, SPC, PFMEA and environmental control procedures — proving the shop runs documented, automotive-grade process control on actual jobs rather than only in a manual.
Machining Factory Quality — Related Pages
Continue reading: Machining Factory · Machining Factory · Machining Factory Services
Standards referenced on this page
- IATF 16949:2016 — Automotive quality management system standard
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars